


-

2-Layer Air Bubble Film Machine (2-Extruder)
3
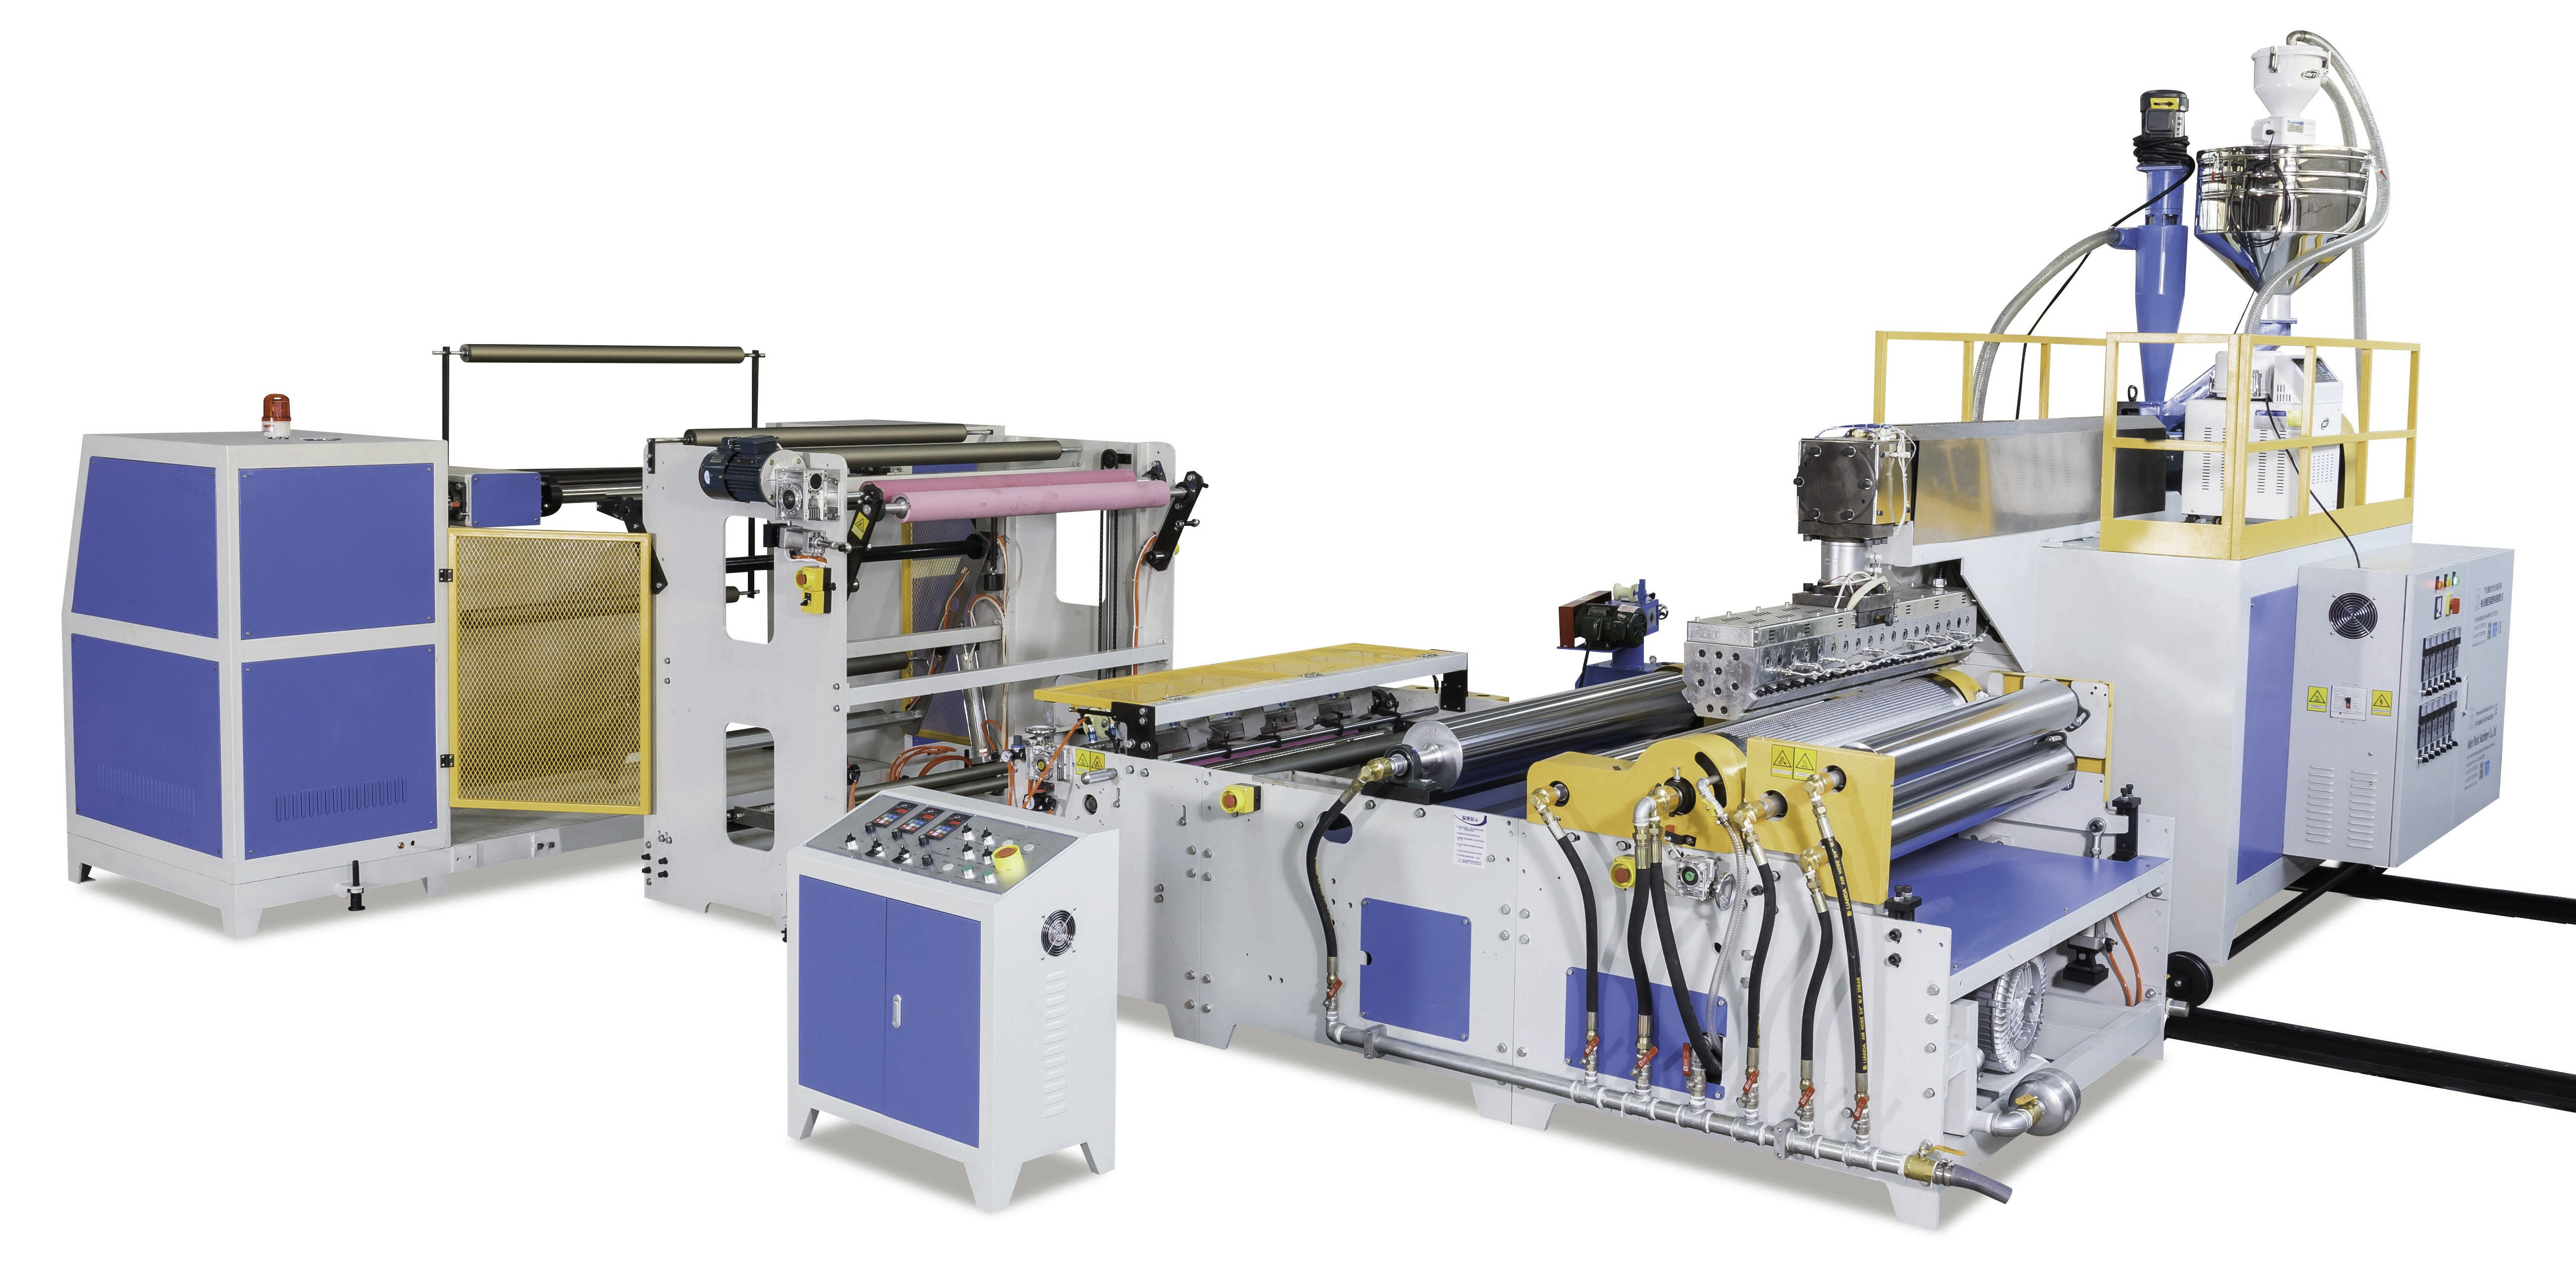
2-Layer Air Bubble Film Machine (Single Extruder)
4

3-Layer Air Bubble Film Machine (2-Extruder)
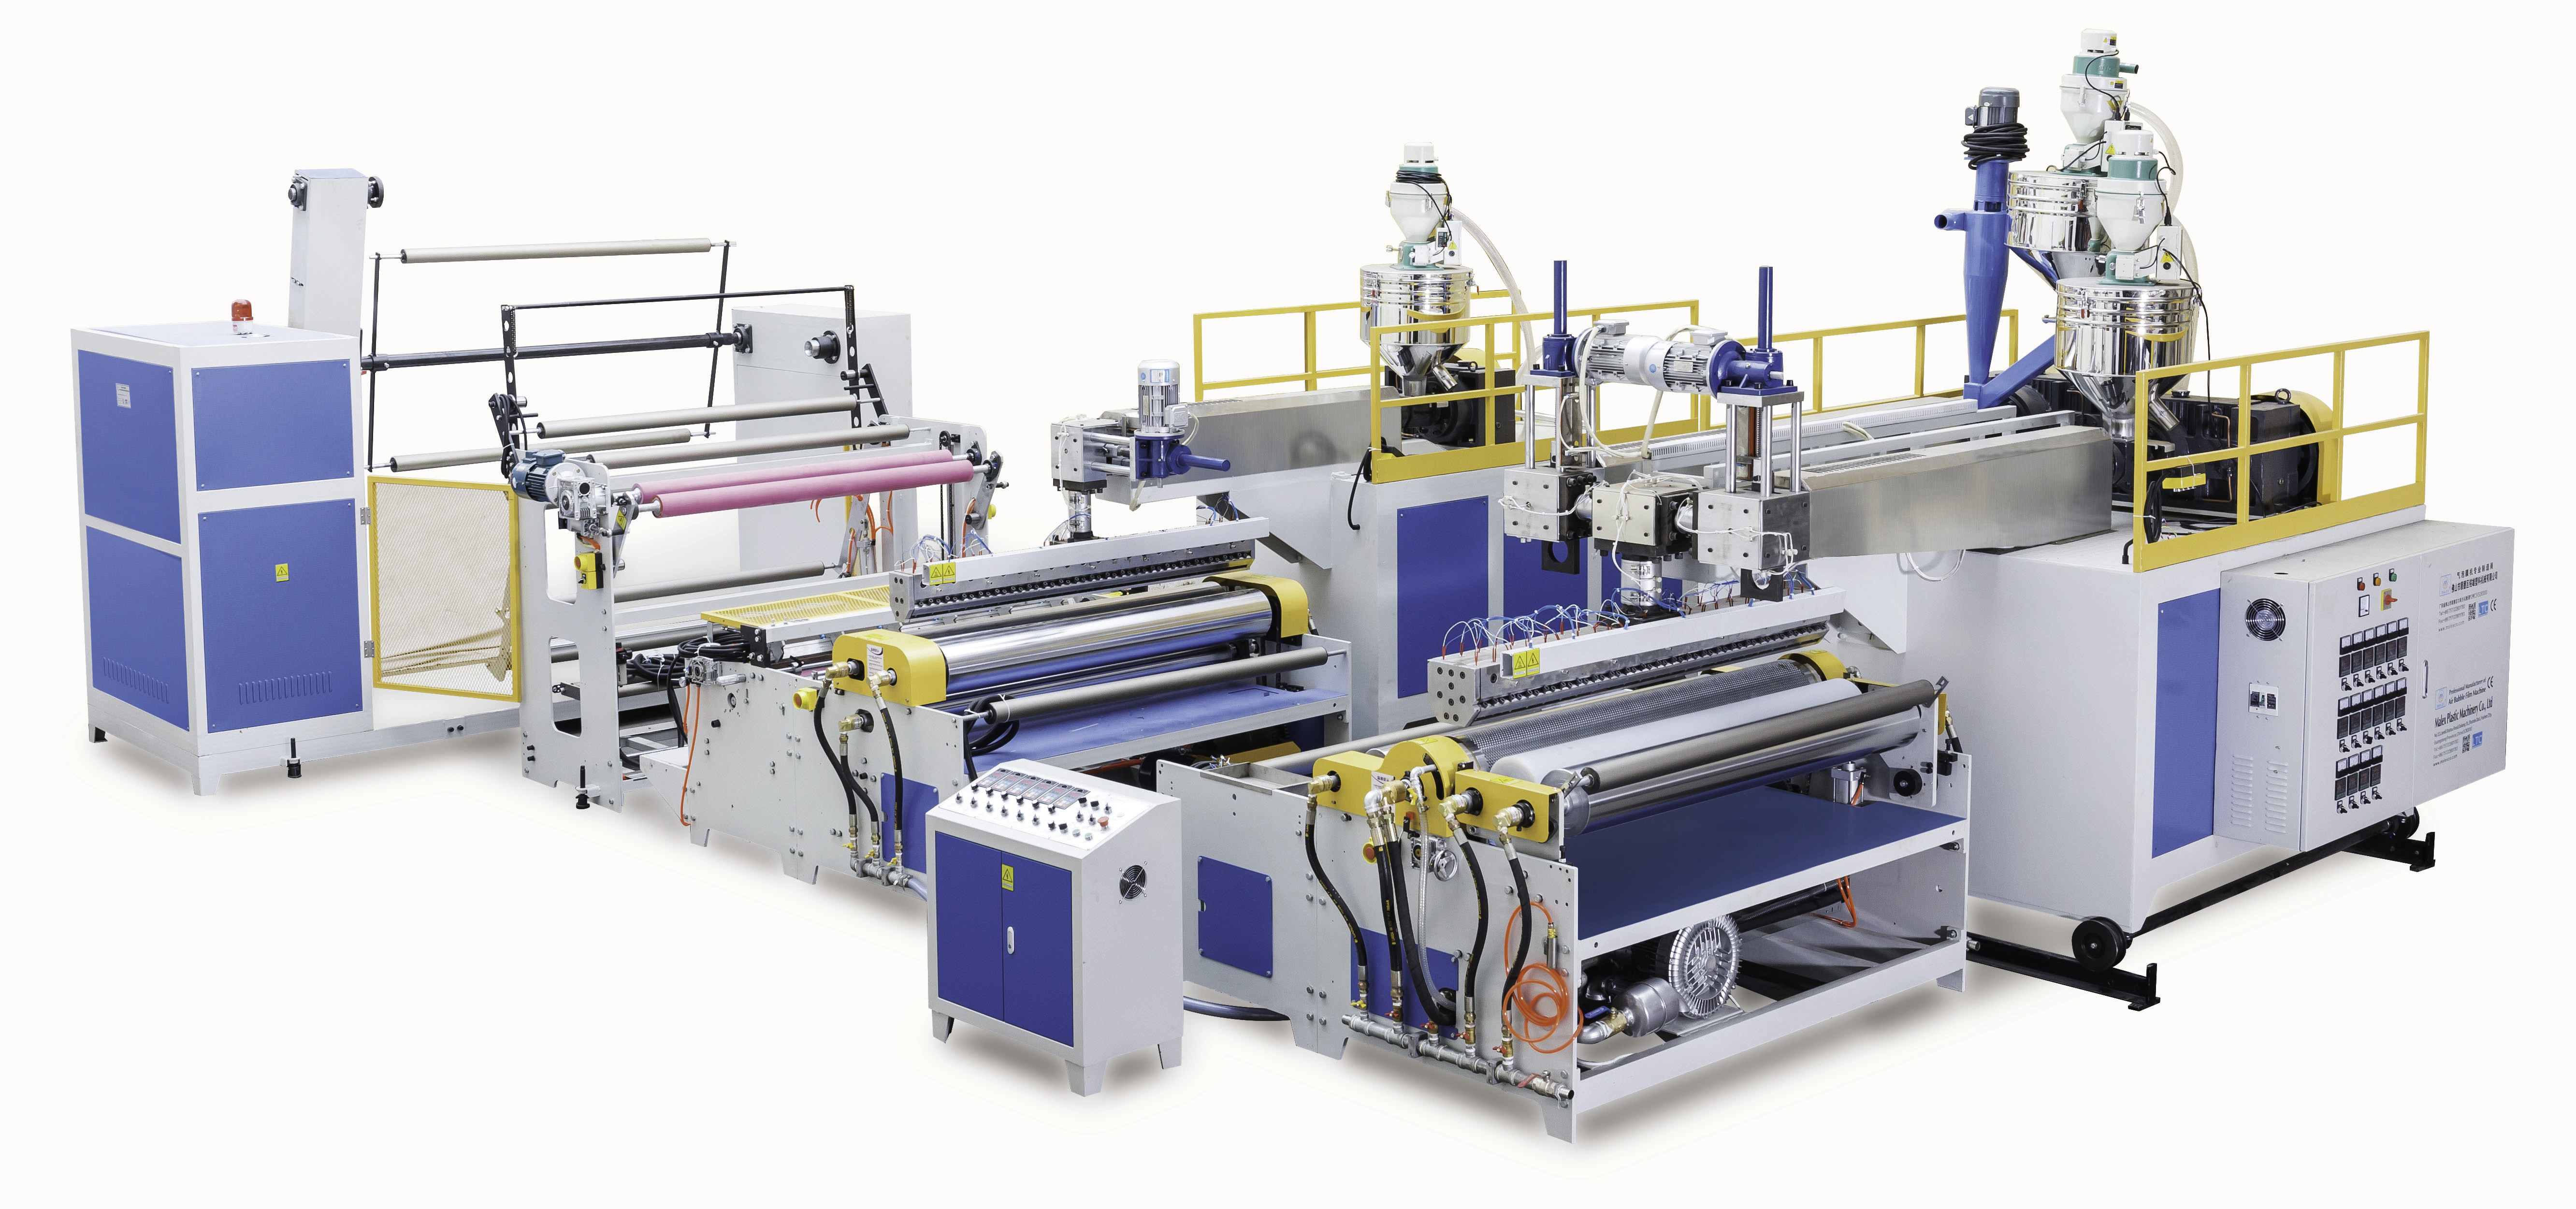
3-Layer Air Bubble Film Machine (3-Extruder)
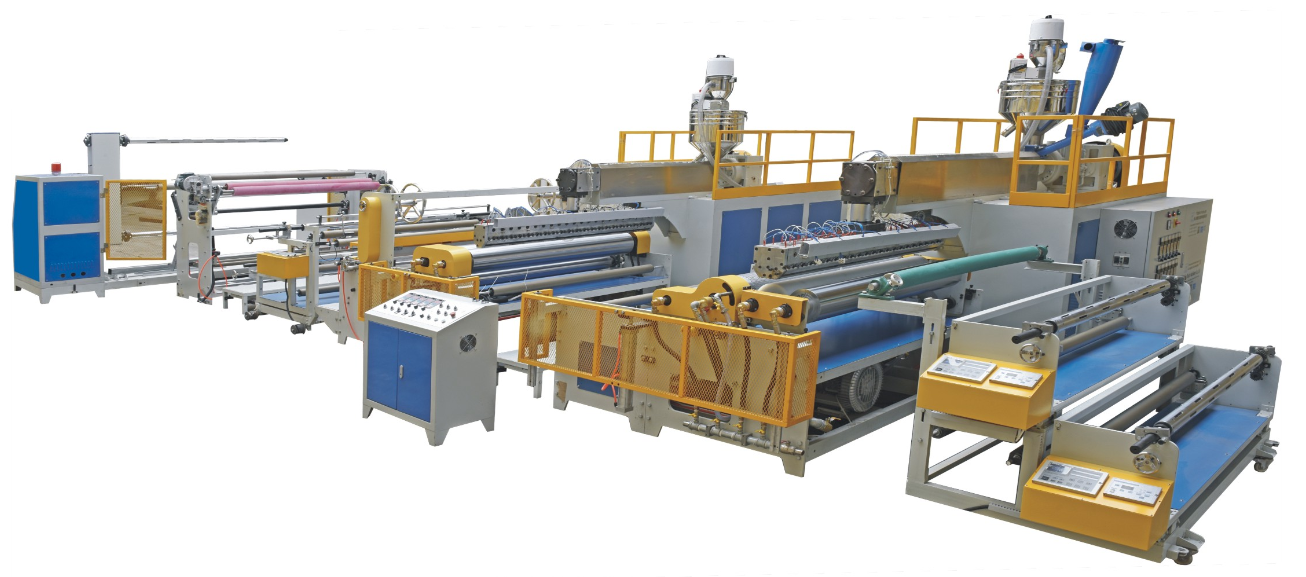
5-Layer Air Bubble Film Machine (2-Extruder)
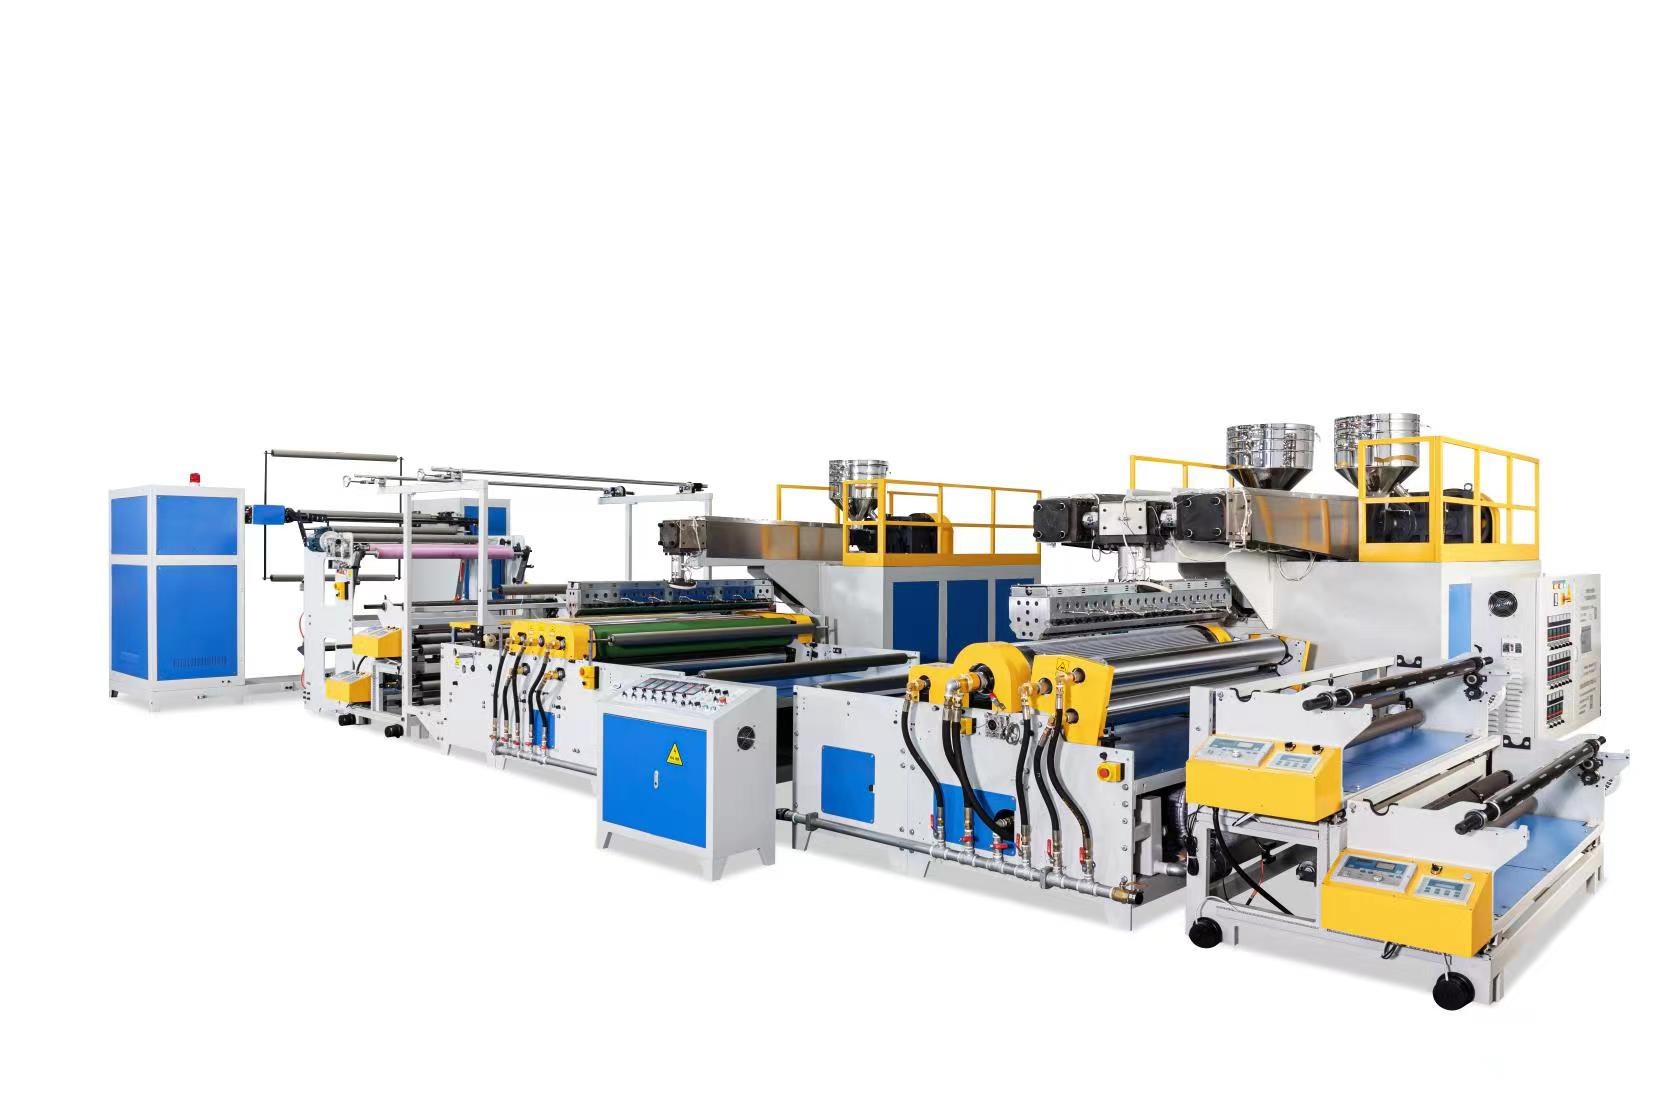
5-Layer Air Bubble Film Machine (3-Extruder)

7-Layer Air Bubble Film Machine (3-Extruder)
7-Layer Air Bubble Film Machine (5-Extruder)
-
-




Dec 23,2024
Understanding the Advantages of 5 Layer Air Bubble Film Machine in Packaging
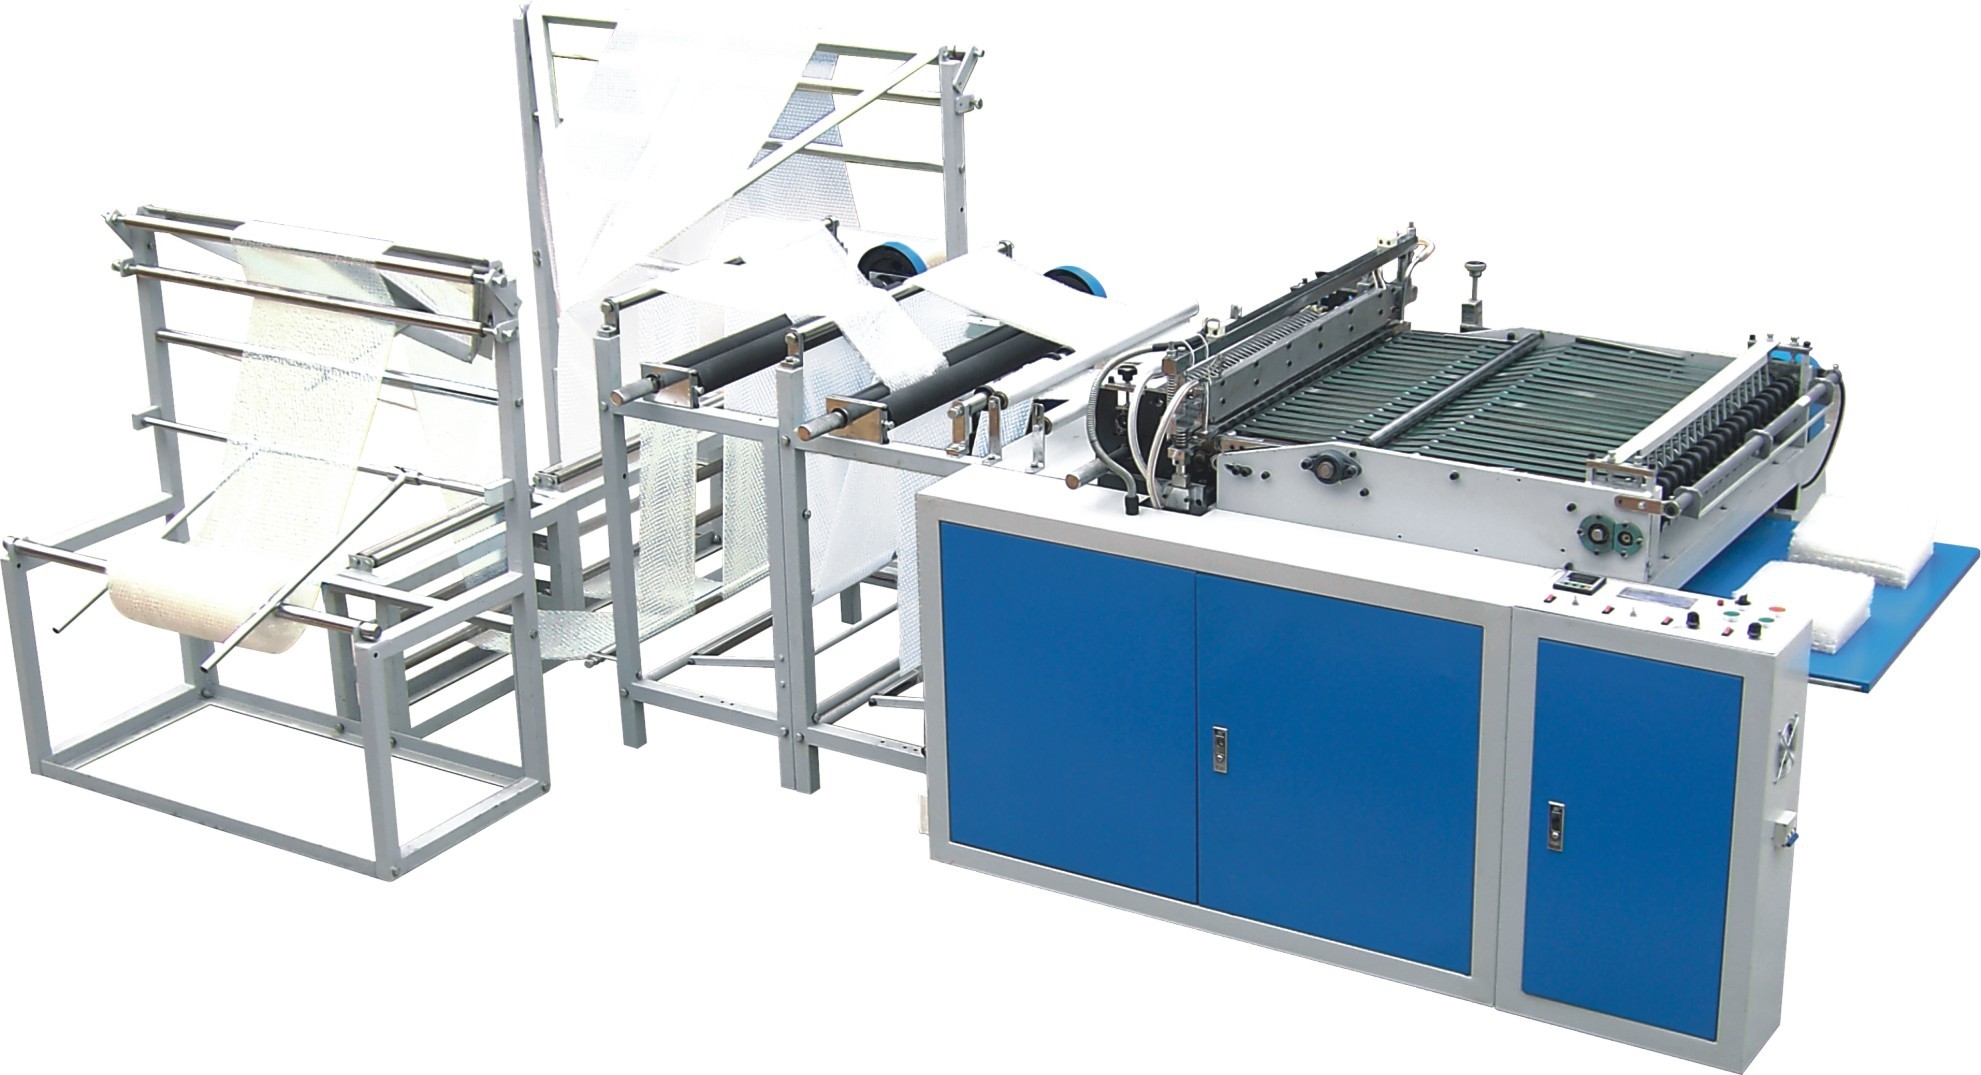
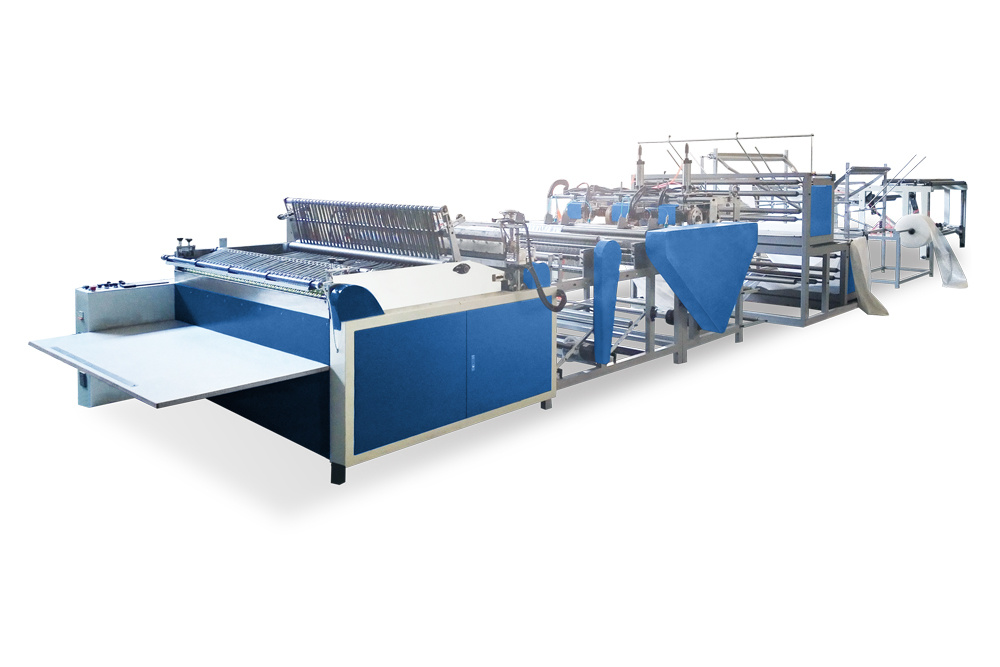
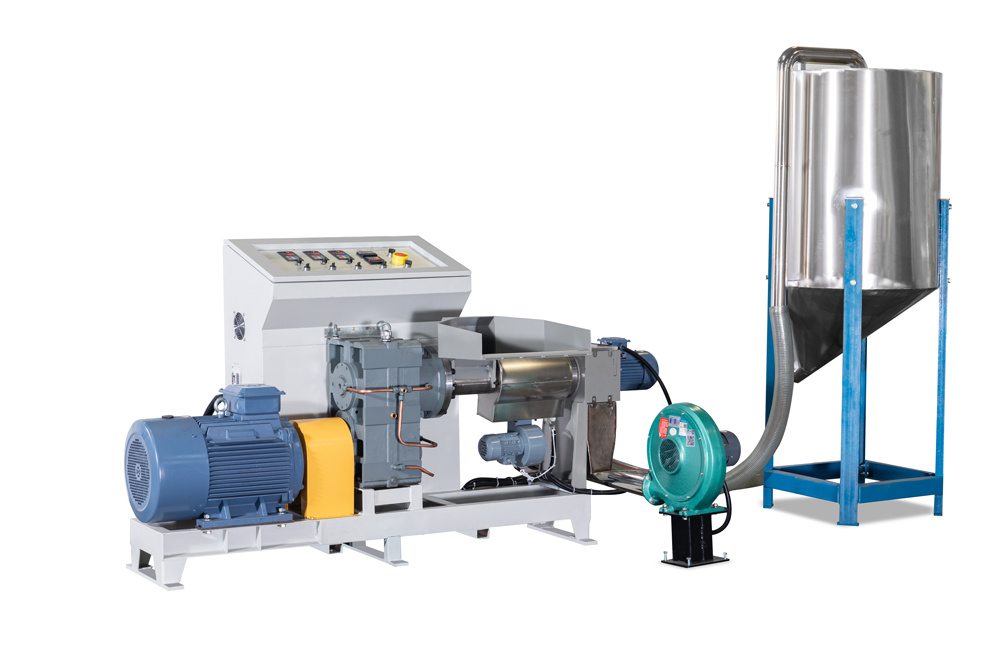
In the realm of packaging machinery, the 5 Layer Air Bubble Film Machine stands out as a crucial innovation that significantly improves the quality and efficiency of protective packaging. This machine is specifically designed to produce multi-layer air bubble film, which is widely used in various industries for safeguarding delicate items during transportation and storage. Understanding how this machinery operates and its benefits can greatly assist professionals in making informed decisions regarding packaging solutions.
The primary function of the 5 Layer Air Bubble Film Machine is to create air bubble film that consists of multiple layers, typically five. Each layer plays a role in enhancing the film's strength, durability, and cushioning properties. The unique structure of this film ensures that it effectively absorbs shock, which is essential for protecting fragile products such as electronics, glassware, and more during shipping.
One significant advantage of using a 5 Layer Air Bubble Film Machine is the enhanced protection it offers. The air-filled bubbles act as a cushion, preventing damage from impact and vibrations. This feature is particularly beneficial in industries where product integrity is paramount, such as pharmaceuticals, electronics, and fragile goods. By utilizing this type of packaging, businesses can reduce the risk of product returns due to damage, thereby improving customer satisfaction.
Moreover, the efficiency of the 5 Layer Air Bubble Film Machine contributes to cost savings. The machine's ability to produce high-quality bubble film in large quantities allows manufacturers to meet demand without compromising on quality. This efficiency not only streamlines production processes but also minimizes waste, which is a growing concern in today’s eco-conscious market. Additionally, the lightweight nature of air bubble film can lead to reduced shipping costs, as lighter packages often incur lower freight charges.
Another aspect to consider is the versatility of the 5 Layer Air Bubble Film Machine. It can be adapted to create various thicknesses and bubble sizes, catering to different packaging needs. This flexibility ensures that businesses can customize their packaging solutions to suit specific products, enhancing their overall packaging strategy.
Furthermore, advancements in technology have led to improved automation and user-friendly interfaces in modern 5 Layer Air Bubble Film Machines. These enhancements facilitate easier operation, maintenance, and integration into existing production lines, making them a smart investment for manufacturers seeking to upgrade their packaging capabilities.
In conclusion, the 5 Layer Air Bubble Film Machine represents a significant advancement in packaging technology. Its ability to produce high-quality, multi-layer air bubble film not only ensures superior protection for products but also offers operational efficiencies that can benefit manufacturers across various sectors. By understanding the advantages of this machinery, businesses can make informed choices that enhance their packaging processes and improve their overall service delivery.
The primary function of the 5 Layer Air Bubble Film Machine is to create air bubble film that consists of multiple layers, typically five. Each layer plays a role in enhancing the film's strength, durability, and cushioning properties. The unique structure of this film ensures that it effectively absorbs shock, which is essential for protecting fragile products such as electronics, glassware, and more during shipping.
One significant advantage of using a 5 Layer Air Bubble Film Machine is the enhanced protection it offers. The air-filled bubbles act as a cushion, preventing damage from impact and vibrations. This feature is particularly beneficial in industries where product integrity is paramount, such as pharmaceuticals, electronics, and fragile goods. By utilizing this type of packaging, businesses can reduce the risk of product returns due to damage, thereby improving customer satisfaction.
Moreover, the efficiency of the 5 Layer Air Bubble Film Machine contributes to cost savings. The machine's ability to produce high-quality bubble film in large quantities allows manufacturers to meet demand without compromising on quality. This efficiency not only streamlines production processes but also minimizes waste, which is a growing concern in today’s eco-conscious market. Additionally, the lightweight nature of air bubble film can lead to reduced shipping costs, as lighter packages often incur lower freight charges.
Another aspect to consider is the versatility of the 5 Layer Air Bubble Film Machine. It can be adapted to create various thicknesses and bubble sizes, catering to different packaging needs. This flexibility ensures that businesses can customize their packaging solutions to suit specific products, enhancing their overall packaging strategy.
Furthermore, advancements in technology have led to improved automation and user-friendly interfaces in modern 5 Layer Air Bubble Film Machines. These enhancements facilitate easier operation, maintenance, and integration into existing production lines, making them a smart investment for manufacturers seeking to upgrade their packaging capabilities.
In conclusion, the 5 Layer Air Bubble Film Machine represents a significant advancement in packaging technology. Its ability to produce high-quality, multi-layer air bubble film not only ensures superior protection for products but also offers operational efficiencies that can benefit manufacturers across various sectors. By understanding the advantages of this machinery, businesses can make informed choices that enhance their packaging processes and improve their overall service delivery.
Related News